Capabilities
Sand casting
Sand casting suits everything from small brackets to large, heavily cored housings, and patterns cost a fraction of permanent mold or die-cast tooling. We run both green sand and air-set (no-bake).
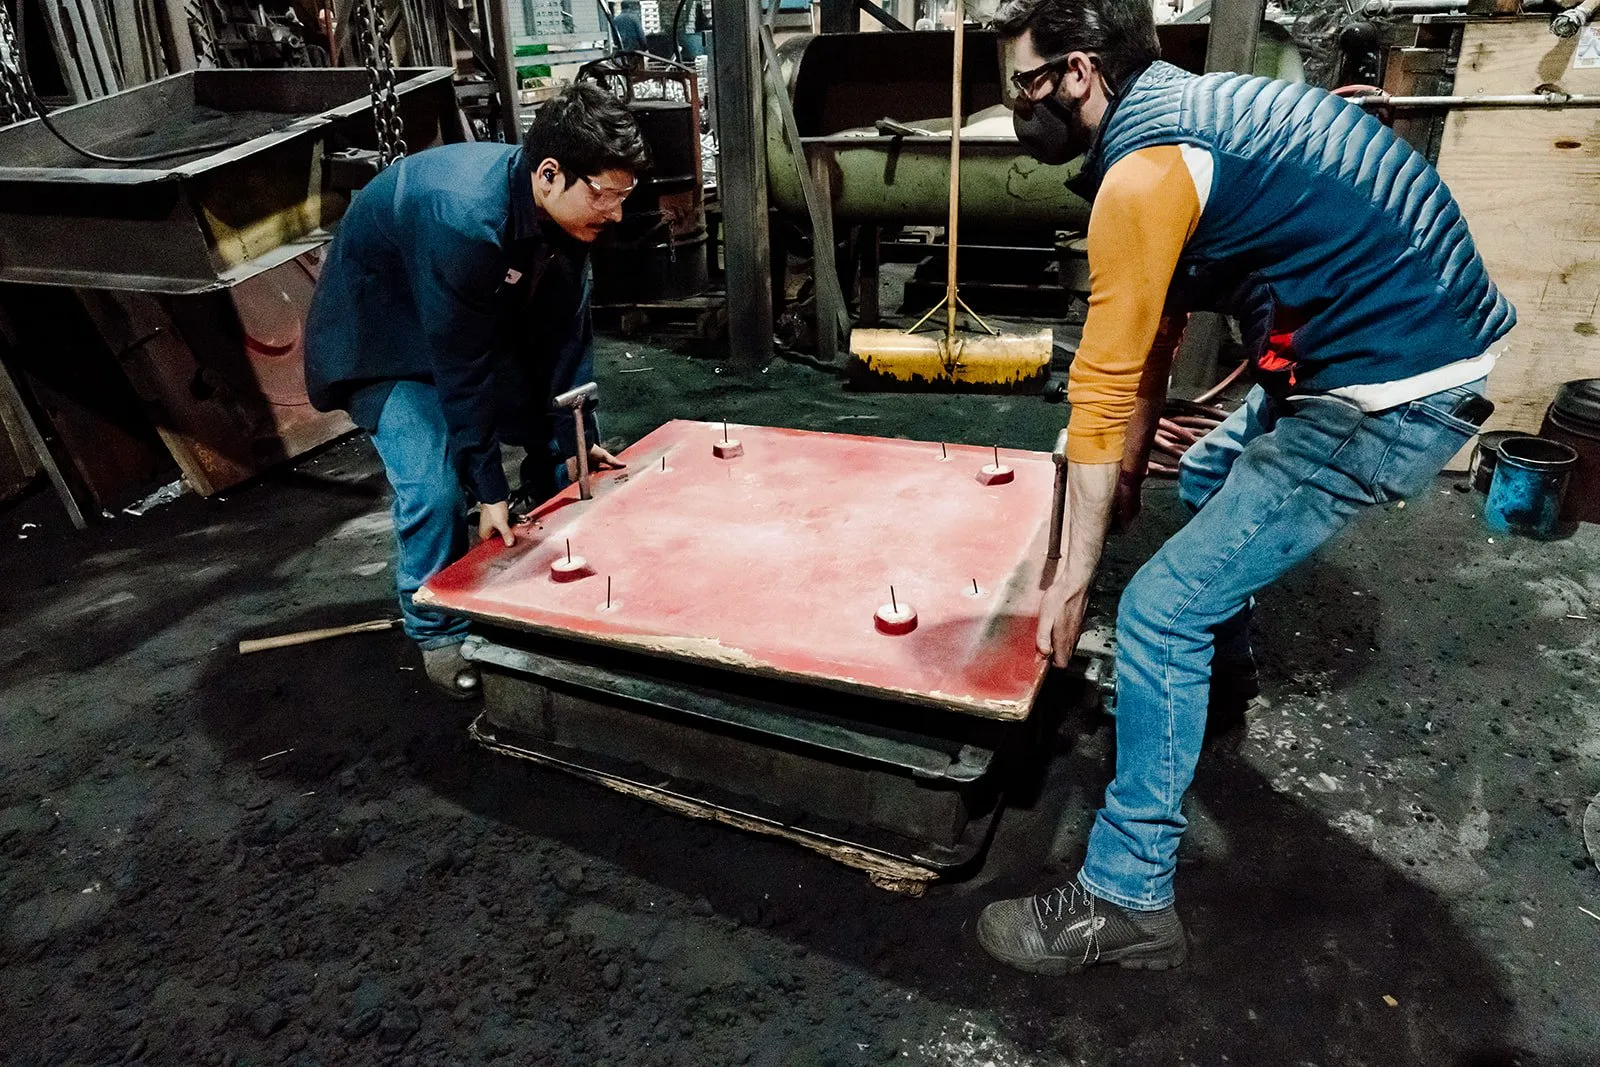
Green sand starts with a pattern, machined or 3D printed. Sand is packed around both halves, cores go in to form hollow features, and the two halves are closed and poured. Afterwards the sand is broken away and reclaimed, and the casting is heat treated, cleaned and finished as needed.
Air-set (no-bake) molds use chemically bonded sand that cures rock hard. It is the right choice for larger castings, complex configurations and very low volumes, often with a turnaround of a few weeks. We use virgin sand for the best surface finish sand casting allows.
Because a sand mold can take a large pour, one casting can often replace an assembly of fabricated parts.
More capabilities
- Permanent moldGravity-fed die casting for repeat parts with tighter tolerances and a better finish than sand.
- CNC machiningIn-house CNC turning and milling, planned together with the casting.
- Heat treatmentCertified furnaces bring castings to the strength your print calls for, in-house.
- FinishingCastings cleaned, ground and blasted, ready for machining, coating or assembly.
- Prototypes & toolingCast aluminum prototypes in about a week, and tooling built and maintained in-house.
Related reading
Metal Sand Casting Process—Step-by-Step
Precision Sand Casting in 6 Steps. Sand casting is pouring molten metal into a sand mold; the metal then solidifies to fill the shape of the mold. While proper equipment and experience are required to produce a casting free of defects, the sand casting process itself is pretty simple.
Read the article →3 Types of Sand Casting
Over 70% of the world’s metal castings are produced via the sand-casting process. Sand casting is highly efficient and cost-effective.
Read the article →A Guide To Non-ferrous Metal Alloy Casting
Metal casting is a complicated process that involves pouring liquid metal into a mold, allowing it to cool, and then extracting the product. Depending on the metal used and the required outcome, we utilize sand casting or permanent mold casting to create prototypes and products. Non-ferrous sand casting is highly efficient and cost-effective. Permanent mold utilizes gravity when pouring molten aluminum into molds (or dies) machined from cast iron or steel. Ermak takes pride in producing high-quality castings that are consistent, repeatable, and cost-effective. We customize the casting process to meet your needs using the best, most efficient non-ferrous metal casting process for your product.
Read the article →
Have a drawing? Get a quote.
Tell us about your part, or just send the file. A real person reviews every request.